metal 3D printing

What can be manufactured with an ALBA?

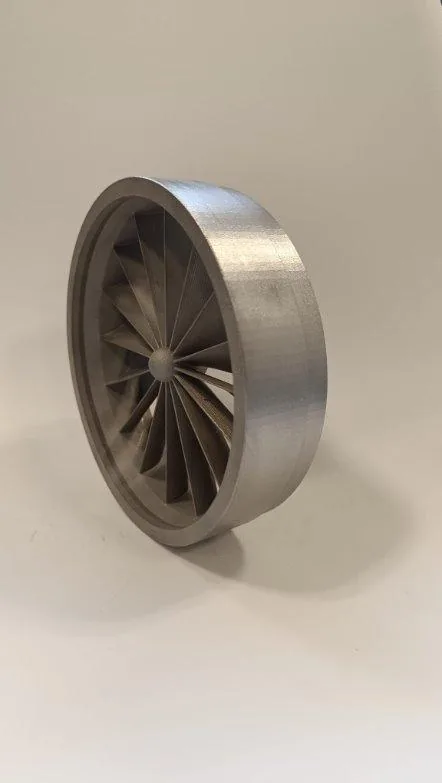
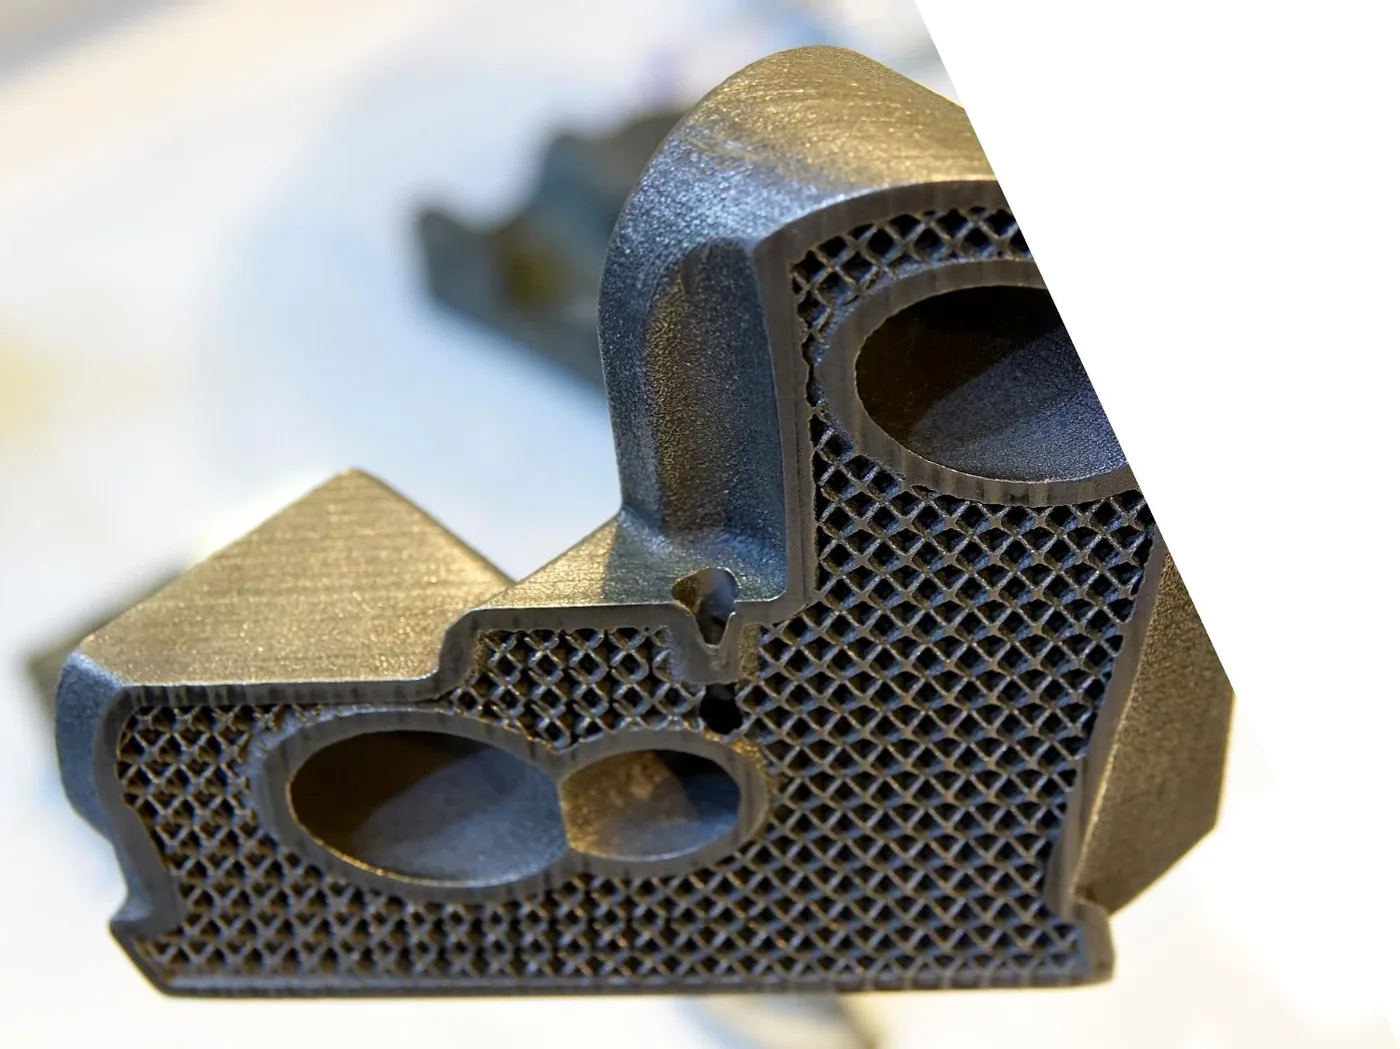
3D metal printing by laser powder bed fusion: closed impellers, seamless collectors, conformal cooling inserts and lattice structures that no other technique can achieve.

Everything underneath are real parts manufactured with an ALBA 300 or an ALBA 500. None of them are renders.

Hover your mouse over any of them to see them more closely.

Set of parts manufactured by metal 3D printing: collector, lattice structure, topologically optimized fork and plates
metal 3D printing Part families Collector, lattice structure, optimized fork, and exchange plates. All from the same machine.
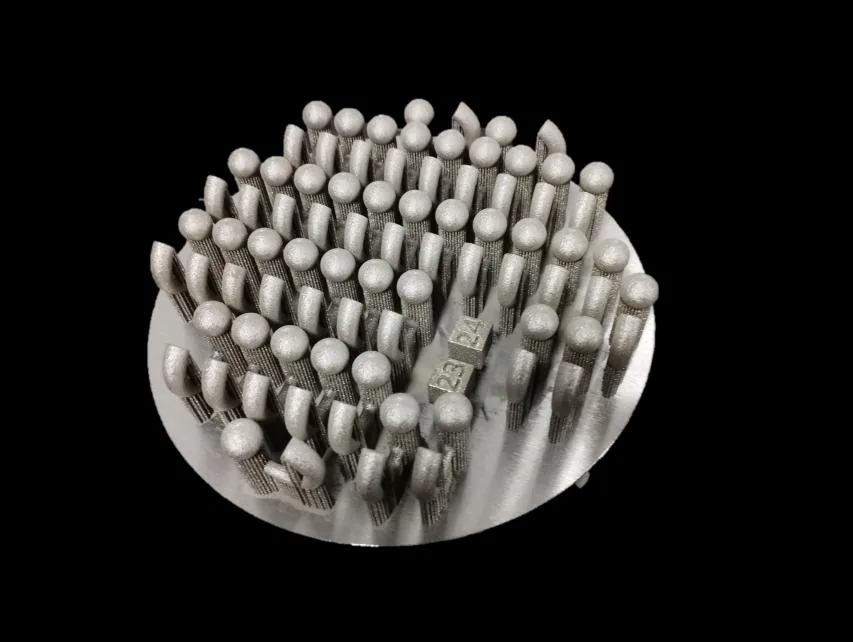
Metal-printed structural part on the platform, still with its lattice supports
Manufacturing supports Fresh from the build chamber With its lattice supports still in place. This is what a part actually looks like before it's separated and cleaned.
Closed turbomachine impeller printed in metal with polished finish
One-part turbomachine Closed impeller Internal blades and housing are a single part. No tools can go in there.
Three turbine impellers of different sizes manufactured by metal 3D printing
Short series in metal Three sizes The same geometry in three scales. Changing sizes doesn't require new tooling.
Detail of metal printed parts with internal lattice structure and manufacturing surface
internal lattice structure The close-up detail Lattice, through-holes, and machined surface. The fine finishing comes later, only where the drawing calls for it.
Heat sink with thin radial fins manufactured by metal 3D printing
Cooling and dissipation Finned heatsink Thin fins, very close together, impossible to machine. The heat exchange surface is determined by the heat sink, not the milling cutter.
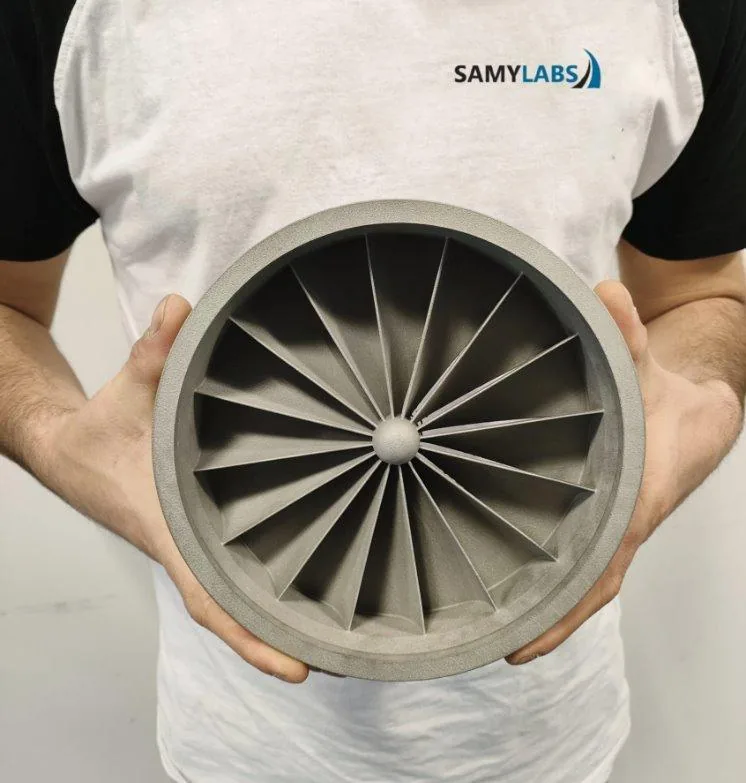
Turbomachine wheel printed on metal, held with both hands
metal 3D printing Turbomachine impeller Printed in one part, without assembly or welding. The internal blades are positioned where no tool can reach.
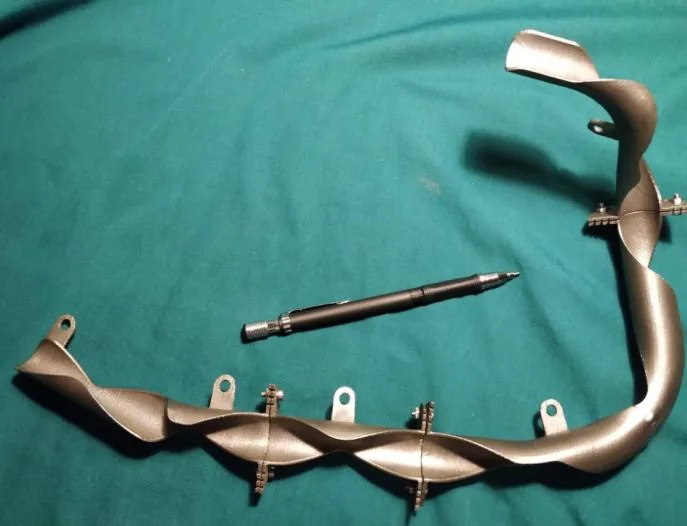
Monolithic tubular manifold printed in metal by laser powder bed fusion
Internal channels formed Monolithic tubular collector Seamless and leak-free. The fluid determines the path, not the drill bit.
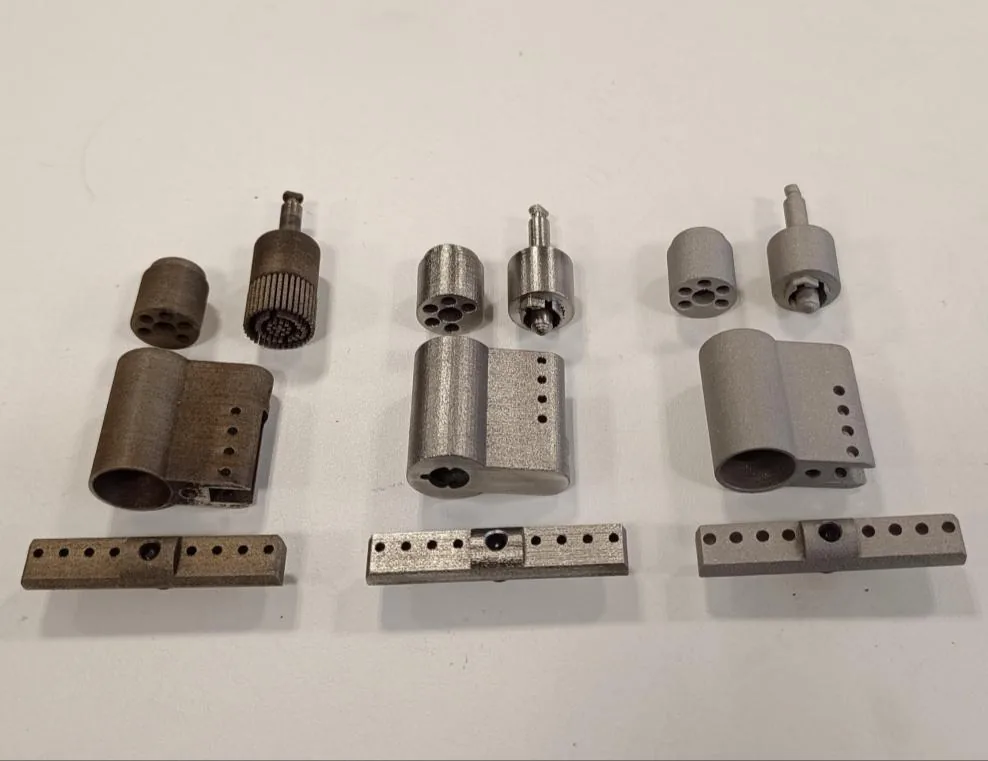
Metal inserts and bushings with conformal cooling manufactured by additive manufacturing
Conformal cooling Inserts and bushings Internal channels that follow the cavity surface: less cycle time and less deformation.
metal-printed lightening lattice structure
Topological lightening Lattice structure Material only where the load demands it. The same rigidity at a fraction of the weight.
Macro photograph of a lattice structure printed on metal
Layers of 20 to 100 microns Grid detail Lightweighting and heat exchange in the same part. Here you can see the grain of the process with the naked eye.
Metal-printed turbine blades and impellers
Non-machinable geometries Blades and rollers Turbomachinery in short series, without tooling and without mold lead time. AlSi10Mg
3D printed metal nozzle as a functional prototype
Functional metallic prototype Nozzle From the file to the tested part in days. It's tested on metal, not plastic.
4-in-1 exhaust manifold, printed on metal and mirror polished
Printed monolithic collector 4-in-1 exhaust manifold The four tubes come out in one part and are then polished. Not a single weld in the gas path.
Lightweight structural part with internal grid structure filling printed in metal
internal lattice structure Lightweight structural component The cut reveals the lattice. Removing material where it's not needed is the most direct way to reduce weight.
Conical diffuser with radial vanes manufactured in metal by laser powder bed fusion
One-part blades Diffuser with radial blades The entire crown comes out as one part. Unassembled, unwelded, and without assembly tools.
Cylindrical diffuser nozzle with internal holes, 3D printed in metal
Internal ducts Diffuser nozzle The internal holes cannot be drilled: there is nowhere to get the tool in.
Mold insert with conformal cooling: CAD model and part manufactured by metal 3D printing
Conformal cooling Mold insert The model and the actual part. The channels follow the cavity at a constant distance.
Nozzle with fine mesh head manufactured by metal 3D printing on the build platform
Detail below the millimeter Fine mesh head Fresh out of the machine, still on the platform and undusted.
Miniature tower with very fine latticework, 3D printed in metal
Precision in 3D metal printing Thin section lattice Bars of very small cross-section that stand upright. It's proof of the level of detail.
Crowns and helical gears manufactured by metal 3D printing
Metal-printed gears Crowns and helical gears Direct machine toothing. The fine finishing comes later, only where the drawing requires it.
Tapered toothed crown printed in metal by laser fusion
Spare parts on demand Conical toothed crown Without tooling to amortize, a unit costs what it costs to manufacture it.
Synchronizer-type toothed ring manufactured by metal 3D printing
Discontinued item Ring with perimeter teeth The kind of spare part that nobody makes anymore, and which is worth its weight in gold for a machine that's out of service.
Cam with internal teeth 3D printed in metal
Short series in metal Cam with internal teeth Complete internal geometry, without chained machining operations.
Curved blades printed in metal on their support structures on the platform
Manufacturing supports Blades on supports This is how they come out of the chamber. The number of supports needed depends on the orientation.
Parts with clamps and support structures on the platform of an ALBA printer
Metal additive manufacturing Parts with clamps Still anchored to the platform. Separating them and cleaning the supports is a person's job.
Machined disc on the build platform of a metal 3D printer
LPBF 3D Printing Revolved part On the platform, before the wire EDM that separates it.
Wine corks marked with a stamp manufactured by metal 3D printing
Marking tools Marked corks The product is not the part: it is what the part leaves marked, thousands of times.
Mirror-engraved metal marking stamp manufactured by 3D printing
Mirror engraving Marking stamp Each order is a different geometry. Precisely where a conventional mold isn't cost-effective.
3D printed metal branding plate with embossed shields
Fine relief on metal Embossed plaque Detail of tenths of a millimeter sustained across the entire surface.
Metal branding stamp with embossed logo and shields
Custom branding Stamp with logo Inverted logo, ready for hot stamping.
Two mold halves with cavities manufactured by metal 3D printing
Printed tooling Mold body Two halves with integrated cavities, without added inserts or parts.
Build build plate with metal-printed lattice structure test specimens
Material characterization Lattice test specimens Several at once in the same build: this is how it is characterized without wasting a build plate per test specimen.
Sample of small 3D printed metal parts held in the hand
Small metal parts Hand sampler Key, gears and a one-time printed articulated part, already assembled.
3D printed metal cutlery with a polished, glossy finish
Mirror finish Polished cutlery The finish is decided after manufacturing: the same part, matte or polished.
Cutlery manufactured by metal 3D printing with a matte finish
Machine finish Unfinished cutlery Just as it comes out, unpolished. It's useful for seeing the actual roughness of the process.
Rocket figure printed on metal and polished to a mirror
Additive polishing Polished curved surface Continuous curvature, polished to a mirror finish. The difficult part isn't printing it, it's finishing it.
Lunar module model with fine structure 3D printed in metal
Metallic print detail Model with fine structure Elements less than one millimeter in size that can be held without deforming.
3D printed winged figure in metal with a polished finish
Free geometry Complex surface figure Sculpture and technical part go through the same process and the same rules.
Miniature part printed on metal held in the palm of the hand
Actual scale Miniature part It fits in the palm of your hand. The scale is misleading in photos without reference.

All the parts in this mosaic have been reviewed and approved by Samylabs. The rule remains in place for future projects: no photo of a real part goes on the website without first being reviewed, even if no client's name appears, because a distinctive geometry identifies the project just as well.

Sample

What's on the table, and you can touch it.

Medical and dental

Hip cups, implants and spinal separators; high-precision crowns and dental parts. Different geometry in each unit and no tooling costs, which is exactly where additive manufacturing wins.

Mold and tooling

Industrial molds and tooling, including tube forming molds, seals and marking tools.

Fluids and thermal

Filters and porous structures optimized for flow, and components with internal channels that no cutting tool can reach.

High temperature

Nozzles, combustion parts and turbine components for applications where the material is hot.

Structure and weight

Topologically optimized parts: material only where the load demands it, with the same rigidity and a fraction of the weight.

Beauty and jewelry

Sculptures, aesthetic parts, and metal jewelry with complex geometries. These are the parts that best explain at a glance the freedom that the process provides.

What if yours is next?

Upload the geometry and we'll tell you the cost and timeframe. If it's not eligible for LPBF, we'll let you know that too.

Sectors

Where it is being used.

Aeronautics and space

Engine components subjected to high temperatures, turbine elements, lightweight parts, and auxiliary components. This is the sector where weight savings pay for themselves.

Industry and automotive

Functional prototypes, discontinued machine parts, and custom components. Manufacturing a discontinued part is usually cheaper than sourcing it.

Mold and die making

Conformal cooled inserts, mold parts, stampings, and complete small molds. The case that most often proves profitable on the first try.

Medical and dental

Prostheses, orthopedic implants and exoskeletons; crowns, bridges, cantilevers and reconstructions. Different geometry in each unit, with no tooling cost.

Education and research

Study of the technology and development of new materials and procedures related to the SLM process. With open parameterization, which is the only way to truly conduct research.

Defense and energy

Manufacturing capacity in our own territory, without depending on an external license to produce a critical part.

To learn more

Design to succeed

The rules that decide whether a part is printed or fought over.

Everything we have written about LPBF →